China Top 10 Programmable V Grooving Machines for Grey Board
Grey board can look simple on a worktable. Cutting it accurately is not. A small depth error may leave a weak hinge, while an uneven groove can make a finished box sit crooked. That is why buyers compare programmable V grooving machines by more than speed or price. They also examine blade adjustment, positioning accuracy, board thickness range, software controls, and after-sales support.
“[Insert a verified industry expert’s name]” puts the practical test plainly: “A groove earns its value when the board folds cleanly and holds its shape.” This quotation should be confirmed with a named, verifiable specialist before publication. It reflects a useful buying principle: judge the cut by the finished fold, not by a brochure specification alone. A Programmable V Cut Grooving Machine For Grey Board should handle repeat jobs consistently, allow operators to set groove positions with confidence, and make routine adjustments clear. Details matter. So does operator training.
This guide introduces ten China-based machines for grey-board processing. It considers their control systems, working formats, cutting performance, and suitability for packaging applications. Product specifications can change, and advertised accuracy may depend on board quality, setup, and maintenance. A comparison is not a substitute for a sample test. Ask suppliers to groove your own material, inspect the fold under real production conditions, and verify service arrangements before making a decision. Some differences are easy to miss on paper. They become obvious on the shop floor.
Grey Board Fundamentals: Caliper Measurement Under ISO 534
Grey board caliper is more than a number on a supplier’s sheet. Under ISO 534, thickness is measured between parallel surfaces using a specified pressure. This matters because board compresses slightly during measurement. A reading from a hand ruler cannot replace a calibrated thickness gauge. Condition samples consistently, then measure several points across each sheet. Edge readings may differ from the center. Small variations can change the material left beneath a V groove.
Tips: Record the measurement location and instrument resolution. Use repeated readings, not one convenient spot. Keep the board flat and clean. It sounds simple. It is easy to rush.
For programmable V grooving, use measured caliper as a setup reference, not as an automatic groove-depth value. The cutter, board density, grain direction, and machine condition also affect the finished hinge. Test a sample, inspect the remaining layer, and adjust in small steps. A groove that looks even from above may still crack when folded. Even experienced operators can miss a local thickness change, so retain the measurement record beside the machine settings. A little uncertainty remains; that is a reason to verify, not to guess.
Programmable V-Groover Design: CNC Feed, Blade, and Groove Geometry
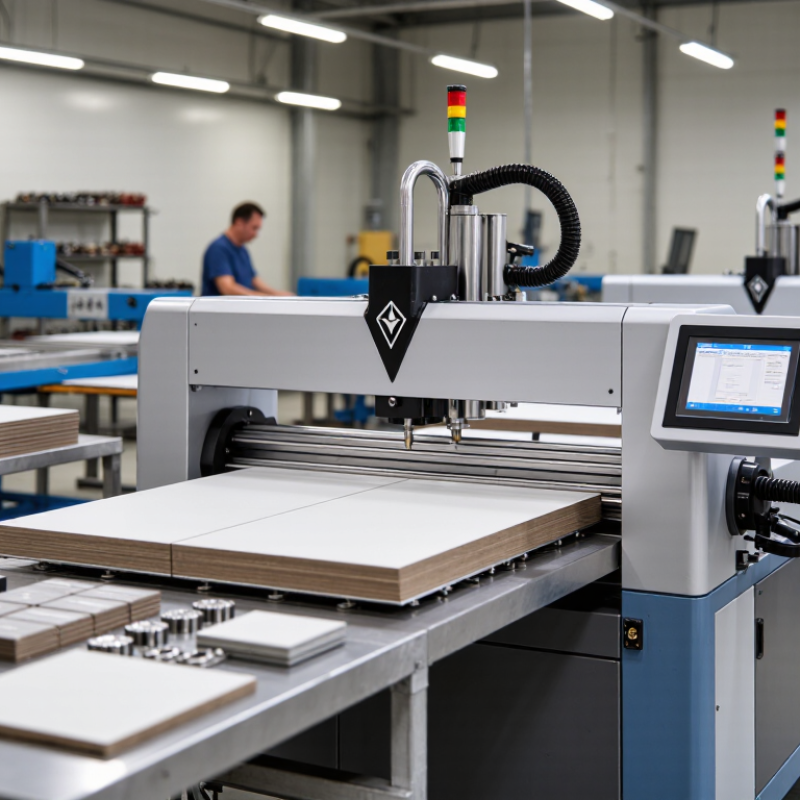
A programmable V-groover is only as accurate as its feed, blade setup, and board measurement. Greyboard can vary in density and thickness, even within one batch. Measure the sheet at several points, then set the CNC feed and cutting depth to suit the actual stock. A sudden speed increase can pull fibres at the groove edge. Watch the surface closely.
CEPI’s Key Statistics 2023 reports that packaging grades made up 62.8% of European paper and board production. That scale reflects broad material demand, not uniform board properties. For machine setup, use a sharp blade and a trial cut to check the remaining hinge layer. A groove that is too deep may crack when folded; one that is too shallow can resist a crisp 90-degree bend. Test the cut. Record blade angle, feed rate, and groove spacing for repeat jobs, then verify them after blade changes. A neat first sample can still hide variation across the sheet. Perfect repeatability is not automatic.
How to Compare 10 Chinese Models: Accuracy, Speed, and Board Thickness
Comparing ten Chinese programmable V-grooving machines requires more than reading the headline accuracy figure. Ask each supplier for positioning accuracy and repeatability test results, measured across the working table rather than at one convenient point. ISO 230-2:2014 describes methods for testing numerically controlled machine-tool positioning accuracy. Use a consistent test method when comparing quoted values. Small differences matter: a groove shifted by even a fraction of a millimeter can affect folding alignment on a rigid grey-board cover.
Speed figures need context. Compare actual boards per hour, including loading, tool changes, and setup—not just the fastest stated feed rate. Then check the permitted board-thickness range against your own stock. ISO 534:2011 specifies a method for measuring paper and board thickness, helping teams record incoming material consistently. Ask for a trial using your board, groove spacing, and required depth. Request sample pieces and note edge cracking, residual hinge thickness, and repeatability. Supplier specifications alone cannot prove production performance.
Tips: Build one comparison sheet for all ten models. Record test conditions, usable table width, thickness range, cycle time, and measured groove deviation. If a figure has no test method, mark it “unverified.” It is a little tedious. Still, it prevents a fast machine from looking better simply because its quoted cycle excludes setup time. ISO 230-2 and ISO 534 provide useful reference methods; confirm the latest editions before formal acceptance testing.
China’s Top 10 Programmable V-Grooving Machines: A Spec-by-Spec Review
A spec-by-spec review of ten programmable V-grooving machines for grey board should begin with usable working width and board thickness. These figures determine whether a machine can handle common panel sizes without extra trimming. Check the groove-depth range and angle settings, too. A narrow adjustment range may limit the folds your workshop can produce.
Control and repeatability matter just as much. Compare how each machine stores cutting programs, sets groove spacing, and adjusts feed speed. Ask for a tolerance figure, then test it on your own grey board; stated accuracy may not match results on warped or uneven sheets. Inspect the blade setup, guarding, and dust extraction. Grey-board fibers can collect around the cutting area, so easy cleaning is a practical advantage. A polished specification sheet is useful, but it cannot replace a sample run.
Tips: Test several board thicknesses. Measure groove depth at both ends, and check whether folded corners stay neat. Record setup time as well as cutting speed. It is easy to overlook setup time, especially when comparing machines during a short demonstration.
Machine Acceptance Testing: Condition Board at 23°C and 50% RH per ISO 187
For acceptance testing a programmable V-grooving machine, condition grey board at 23°C and 50% relative humidity, following ISO 187. Keep test sheets in that atmosphere until their moisture condition stabilizes. The time required can vary with board thickness, packaging, and prior storage. Do not assume a short wait is enough. Record temperature, humidity, conditioning time, and board batch before cutting. A simple digital logger near the samples helps reveal room fluctuations.
Run the conditioned sheets with documented settings for groove depth, spacing, and feed speed. Inspect each groove under consistent lighting for clean edges, uniform depth, and cracking. Then fold the board and check alignment and surface damage. Small differences matter. Use several samples, not just one attractive result, and compare measurements against agreed acceptance limits. A stable room does not erase variation between sheets. Nor does ISO 187 define the machine’s performance limits; those must be set separately. I would not treat one clean fold as proof. If results drift, check the board’s conditioning and the machine setup before changing parameters. Keep the test record with the settings, observations, and any retest notes.
China Top 10 Programmable V Grooving Machines for Grey Board - Machine Acceptance Testing: Condition Board at 23°C and 50% RH per ISO 187
Illustrative acceptance-test comparison of ten generic machine configurations, not verified product specifications or a market ranking. ISO 187 specifies the standard atmosphere for conditioning paper and board; the machine performance limits below are proposed test criteria, not ISO 187 requirements. Condition specimens at 23 ± 1°C and 50 ± 2% RH until moisture equilibrium, and record the actual conditioning time.
| Test ID | Generic machine configuration | Maximum board size (mm) | Board thickness (mm) | Programmed groove angle | Position error limit (mm) | Groove-width error limit (mm) | Test run target (boards/h) | Board conditioning record |
| 01 | Compact single-head, manual loading | 600 × 800 | 1.0–3.0 | 90° | ±0.30 | ±0.20 | 120 | 23.0°C; 50% RH; equilibrium documented |
| 02 | Compact single-head, programmable stop | 700 × 1000 | 1.0–4.0 | 90° | ±0.25 | ±0.20 | 150 | 23.0°C; 50% RH; equilibrium documented |
| 03 | Single-head CNC, fixed-angle tooling | 900 × 1200 | 1.0–4.0 | 90° | ±0.20 | ±0.15 | 180 | 23.0°C; 50% RH; equilibrium documented |
| 04 | Single-head CNC, adjustable groove depth | 1000 × 1400 | 1.0–5.0 | 90° | ±0.20 | ±0.15 | 200 | 23.0°C; 50% RH; equilibrium documented |
| 05 | Dual-head CNC, sequential grooving | 1200 × 1600 | 1.2–5.0 | 90° | ±0.20 | ±0.15 | 240 | 23.0°C; 50% RH; equilibrium documented |
| 06 | Dual-head CNC, automatic board feed | 1200 × 1800 | 1.2–5.0 | 90° | ±0.20 | ±0.15 | 280 | 23.0°C; 50% RH; equilibrium documented |
| 07 | Multi-tool CNC, programmable groove sequence | 1300 × 1800 | 1.5–6.0 | 90° | ±0.18 | ±0.15 | 300 | 23.0°C; 50% RH; equilibrium documented |
| 08 | Wide-format CNC, automatic positioning | 1500 × 2000 | 1.5–6.0 | 90° | ±0.18 | ±0.15 | 320 | 23.0°C; 50% RH; equilibrium documented |
| 09 | Wide-format dual-head, automated loading | 1600 × 2200 | 1.5–6.0 | 90° | ±0.18 | ±0.15 | 350 | 23.0°C; 50% RH; equilibrium documented |
| 10 | High-throughput CNC line, feed and outfeed handling | 1800 × 2400 | 1.5–6.0 | 90° | ±0.18 | ±0.15 | 380 | 23.0°C; 50% RH; equilibrium documented |
Suggested acceptance method: use conditioned grey-board specimens from a documented lot; verify groove position and width at multiple points with calibrated measuring equipment; inspect for tearing, delamination, and unacceptable surface damage; and record actual output over a defined continuous run. Agree final tolerances, sampling plan, and throughput conditions between buyer and supplier before testing.